
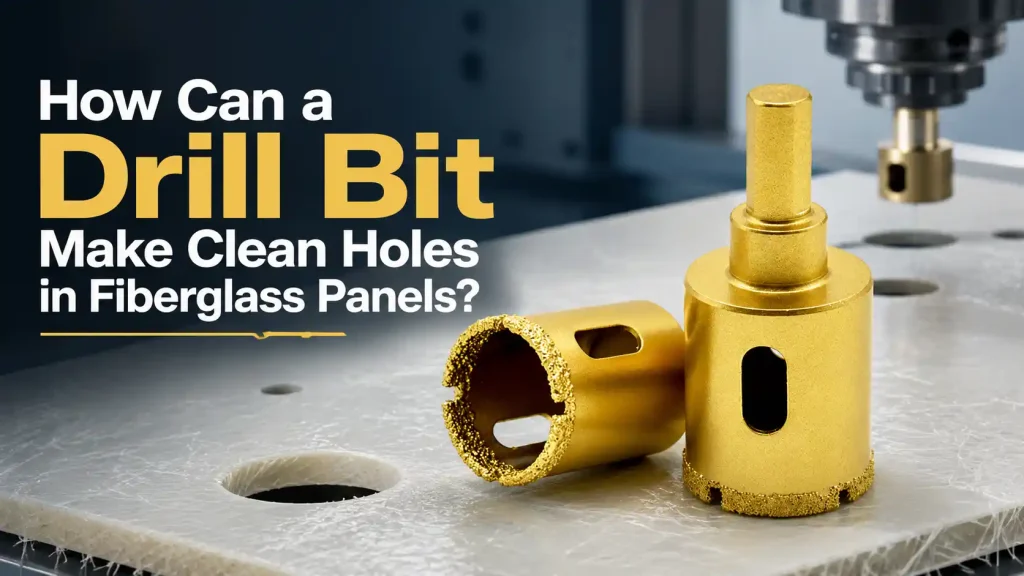
A fiberglass enclosure panel can look flat and uniform before machining, yet the first production holes may expose white fibers, lifted gelcoat, a fuzzy exit edge, or a hidden ring of delamination. The drawing may still show the correct diameter, but the panel is no longer acceptable for sealing, fastener seating, painting, or structural service. A Drill Bit for repeat fiberglass work must therefore be matched to the laminate, hole function, machine interface, support, dust control, and inspection limit as one manufacturing system.
クイックアンサー
A ドリルビット makes clean holes in fiberglass panels when its cutting material, edge condition, point or rim geometry, diameter, working length, shank, and runout are matched to the actual gelcoat, resin, reinforcement, thickness, backing, machine, feed stability, and hole requirement. Clean batch production also depends on controlled support, heat and dust removal, breakthrough behavior, sample approval, wear limits, and inspection for both visible edge damage and subsurface delamination.
Bestwinは、OEM、販売代理店、リピートバッチプログラム向けに、穴あけおよび切削工具を製造しています。Bestwinは、代表的なグラスファイバーパネル、ラミネートの説明、穴の図面、機械の詳細、サイクルターゲット、梱包要件、および年間生産量を基に、予備的なドリルビットの方向性を決定し、特定されたサンプルを準備することができます。リリースされる工具は、一般的な材料ラベルではなく、顧客の実際の複合材からの切削証拠に従う必要があります。

Fiberglass Fails at the Hole Edge Before It Fails in the Drawing
Fiberglass-reinforced plastic is a combination of resin and fibers, not a uniform metal. A surface gelcoat may be harder or more brittle than the laminate underneath. Chopped-strand mat, woven cloth, unidirectional reinforcement, fillers, and local inserts can produce different cutting behavior within the same panel. A sandwich panel can add a foam, honeycomb, or wood core between reinforced skins.
When a Drill Bit enters the top surface, the cutting edge must break the resin without prying up the coating. Inside the laminate, it must sever abrasive glass fibers while carrying resin and fiber fragments out of the hole. Near the exit, the remaining material becomes less supported. Thrust can separate plies or push fibers ahead of the edge before they are cut.
Drill Bit diameter alone may remain within tolerance while these defects grow. Entry chipping can break a sealing surface. Exit fuzz can prevent a washer from seating. Subsurface delamination can enlarge under vibration or moisture exposure. Heat can discolor resin, soften a thermoplastic matrix, or load the edge with smeared material. The inspection plan must therefore describe edge and laminate quality, not only nominal size.
The Panel Construction Defines the Failure Mode
A thin gelcoated cover, a thick hand-laminated enclosure, a pultruded profile, and a high-fiber structural plate do not present the same cutting load. Fiber orientation changes the direction in which damage spreads. Voids or resin-rich areas can also create local variation. A Drill Bit sample should be tested across representative panel locations, including any edge zone or reinforced area that will appear in production.
If the laminate specification is unavailable, retain physical coupons from the actual lot. Record thickness, surface finish, visible reinforcement, and the panel side used as the entry face. Those samples give Bestwin and the customer a shared reference without pretending that every product sold as fiberglass behaves alike.
The Hole Requirement Determines the Cutting Direction
A small clearance hole, a large cable opening, a countersunk fixing, and a hole through a sandwich panel apply different demands to the tool. A conventional twist form may be a reasonable sample direction for some small holes. Spear, brad, multi-facet, abrasive, or annular forms can change entry and exit behavior. Larger diameters may favor a hole-saw style or abrasive rim, but the exact product must still match the laminate and machine.
The Drill Bit must also fit the holder. Straight, reduced, threaded, or other shank forms have different torque transfer and runout implications. Working length should clear the panel and fixture without adding unnecessary overhang. A long Drill Bit can deflect and make one edge carry more load, especially in portable or less rigid equipment.
Table 1. Fiberglass panel hole requirement map
| 穴の状態 | Tool direction to sample | Evidence required |
|---|---|---|
| Small fastener clearance | Sharp point-cutting form with controlled runout | Entry chip, diameter, exit fuzz, washer seating |
| Precision locating hole | Rigid short form and stable guide | Position, roundness, edge quality, repeatability |
| Large cable or gland opening | Annular or abrasive cutting form | Rim quality, plug removal, heat, sealing surface |
| Countersunk fixing | Drilled hole plus controlled secondary geometry | Surface breakout, seat contact, remaining skin |
| Sandwich panel opening | Skin-cutting method matched to the core | Both skins, core pullout, moisture-seal condition |
| Near-edge feature | Low-thrust sample with strong backing | Crack path, edge distance, delamination boundary |
The table is not a universal product prescription. It identifies which Drill Bit form deserves a controlled sample and which part evidence decides whether the direction is acceptable.
A Sharp Edge Must Cut Fibers Without Lifting the Laminate
Glass reinforcement is abrasive. It can round a cutting edge while the tool still looks visually intact. As the edge loses sharpness, thrust and heat rise. Instead of severing fibers cleanly, the Drill Bit can push them into the laminate, pull them from the resin, or leave a fuzzy fringe at the exit.
Drill Bit edge geometry must balance sharpness and support. An extremely delicate edge may cut cleanly at first but chip under runout, interrupted contact, or an unstable machine. A heavily reinforced edge may survive longer but increase thrust. The appropriate balance depends on fiber content, resin, diameter, speed range, fixture rigidity, and the number of holes expected per tool.
点対称性とリム同心性はロット特性です。研磨リムの片方の縁または一部がより強く食い込むと、工具がぶれたり、穴が大きすぎたり、片側が過熱したり、出口に不均一な損傷が発生したりする可能性があります。Bestwin のサンプルレビューは、生産仕様が確定する前に、それらの工具特性と測定された穴の結果を結びつけることができます。
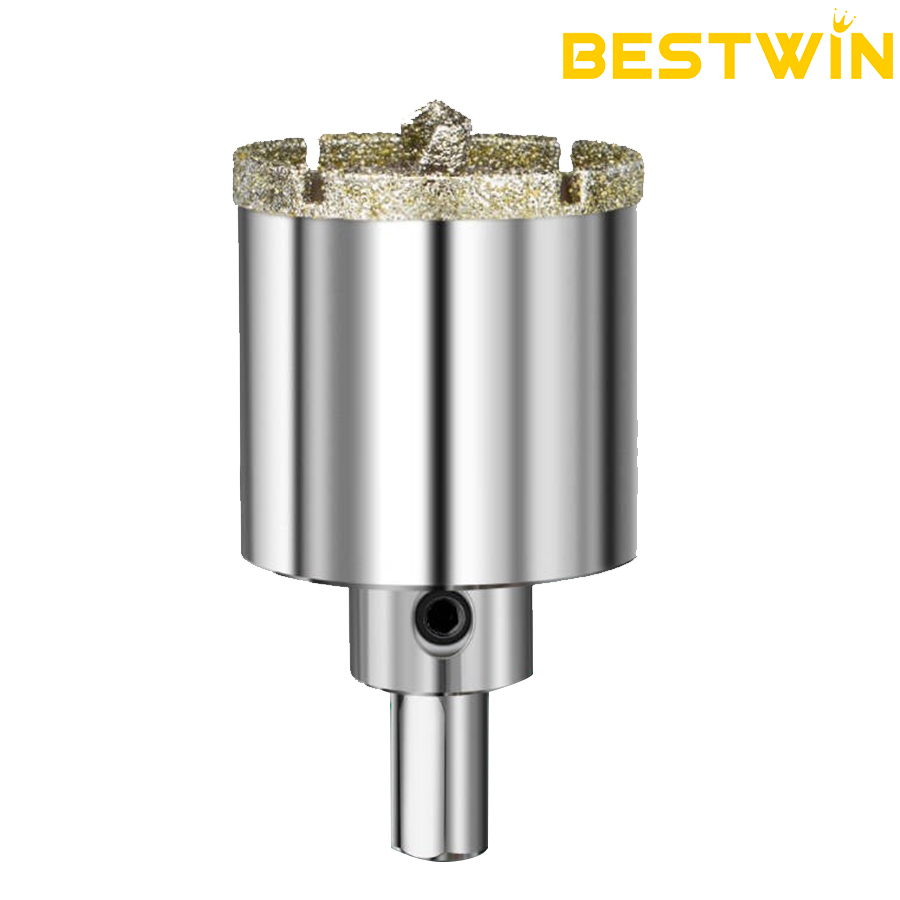
The pictured diamond hole-saw form is an official Bestwin product example of an abrasive annular cutting direction. It should not be treated as automatic approval for every fiberglass panel. Diameter, connection, abrasive specification, machine, laminate, dust method, and sample result remain project-specific.
Heat and Dust Change Both Tool Life and Panel Quality
Fiberglass cutting creates fine abrasive dust and small resin-fiber fragments. If material packs around the edge or inside a hollow cutter, it increases friction and blocks fresh cutting surfaces. Heat then rises at the hole wall. The Drill Bit may begin polishing or smearing rather than cutting, even though the spindle continues to turn normally.
プロジェクトでは、パネル、機械、職場規則と互換性のある抽出、空気移動、ペッククリアランス、湿式制御、またはその他の承認された方法を定義する必要があります。粉塵制御はプロセスおよび安全要件であり、ツールのコーティング主張ではありません。適切な収集装置および個人用保護具は、施設の安全評価および適用される規則に従う必要があります。
Record heat through observable and measurable evidence. Resin discoloration, odor, a glossy bore, material buildup, rising spindle load, or a hot Drill Bit after a fixed cycle can reveal a change. Where temperature is critical, use a defined method and location so that sample lots can be compared. A Drill Bit should not be approved from one clean first hole if heat accumulates across a production sequence.
Cooling decisions require care. A fluid that reduces temperature may contaminate a bonding surface, enter a sandwich core, affect later painting, or conflict with electrical-enclosure cleanliness. A dry process may be required, which places greater importance on edge condition, chip or dust evacuation, duty cycle, and extraction. The released method should represent the real factory process.
Backing and Fixturing Control Exit Damage
The exit side is vulnerable because the remaining laminate becomes thin before the cutting edge completes the hole. If the panel can flex, thrust pushes the last layers away from the tool. Fibers bridge across the opening and tear. A firm, compatible backing surface supports those layers and reduces movement.
Backing must contact the panel without marking the visible face or trapping debris that changes thickness. Replaceable backup material should have a defined condition because a worn or cratered surface no longer supports the Drill Bit exit. For shaped enclosures, the fixture needs to follow the actual geometry rather than forcing the panel flat and introducing stress.
Clamp position is also part of the result. A Drill Bit can cut cleanly near a clamp and produce delamination farther away where the panel vibrates. The sample should include the least-supported production location, not only the easiest center area. Record fixture revision, backing material, clamp spacing, and entry face with the approved hole samples.
Runout at the tool tip or rim magnifies the problem. Its source can be the Drill Bit, adapter, chuck, spindle, debris on the interface, or excess overhang. Checking the assembled system prevents a good tool from being rejected for a machine problem and prevents a machine adjustment from hiding an inconsistent tool batch.
Entry and Breakthrough Need Different Evidence
The entry face reveals how the point or rim starts and centers. A wandering tool can scratch the gelcoat outside the finished diameter. An abrupt first contact can chip a brittle surface. A guide, pilot feature, rigid fixture, or controlled machine path may improve location, but the chosen method must be included in the sample record.
Drill Bit breakthrough reveals thrust, backing, remaining edge sharpness, and fiber cutting. Feed behavior near the exit can change damage, but a production approval should not depend on an operator improvising at every hole. The machine program or documented method needs a repeatable transition that can be trained and audited.
The broad construction of a ドリルビット provides useful terminology for points, flutes, shanks, and cutting edges. Fiberglass approval, however, must be based on the actual composite. Terms that describe a tool do not prove how its edges will interact with a particular gelcoat and fiber architecture.
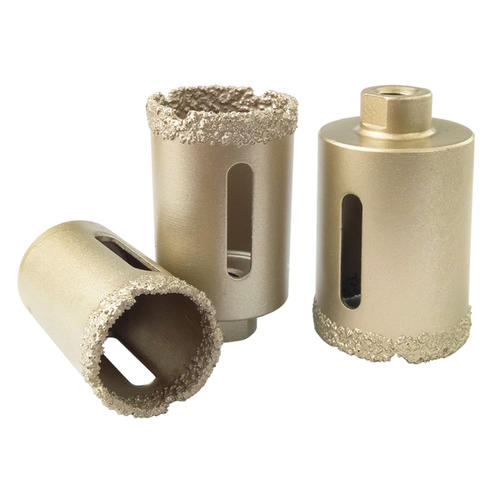
This official M10 brazed diamond hole-saw group illustrates how several diameters can share a product family while still requiring size-by-size verification. Rim speed, contact length, dust space, adapter condition, and panel support change with diameter, so one approved size does not automatically release the whole range.
Factory Matching Starts With the Actual Laminate
Bestwin matches a preliminary tool direction from a representative panel coupon and a completed application record. Useful information includes resin or panel designation, reinforcement type if known, thickness, gelcoat, core construction, hole diameter and tolerance, surface side, edge-distance limit, machine and holder, speed and feed range, extraction method, holes per part, target holes per tool, packaging, marking, and annual volume.
Photographs should include the entry face, bore, exit face, and any delamination visible after sectioning or suitable inspection. Mark the Drill Bit identity and cycle count for each sample. A clean first hole and a damaged fiftieth hole describe a wear trend; without cycle identity, the photographs can be misleading.
This is where a Drill Bit manufacturer connects application evidence with production controls. Bestwin can match or develop a sample direction, define critical geometry and interface details, identify the sample lot, inspect relevant dimensions and edge condition, and preserve the approved identity for repeat supply. The customer remains responsible for validating the tool in the finished process and setting product-specific acceptance limits.
Drill Bit Suppliers sometimes group composite, tile, glass, stone, wood, and metal applications under broad catalog labels. For an OEM fiberglass program, the operational specification must be narrower. Bestwin uses the real panel and hole evidence to define which product family, size, connection, marking, and packaging belong to the released order.
Inspection Must Separate Cosmetic and Structural Defects
Entry chips and exit fuzz are visible, but appearance alone may not reveal a delamination ring below the surface. The inspection method should match the risk of the finished part. A cosmetic cover can have different limits from a structural bracket, pressure boundary, bonded assembly, or weather-sealed enclosure.
Define lighting, magnification, measurement location, sample frequency, and Drill Bit sample pass criteria. Use a reference photograph or retained panel where written descriptions are ambiguous. If sectioning, tap testing, imaging, or another nondestructive method is required, record the method and qualification rather than assuming all inspectors will see the same defect.
Table 2. Fiberglass hole sample and batch release record
| Check | Sample evidence | バッチ制御 |
|---|---|---|
| ツールの識別 | Item code, size, shank, lot, approved sample | Marking and order traceability |
| Entry surface | Chip width, scratches, gelcoat condition | Defined visual reference and sampling |
| Hole geometry | Diameter, roundness, location, wall condition | Calibrated method and inspection frequency |
| Exit surface | Fuzz, breakout, fiber pull, backing condition | Photo standard and replacement limit |
| Delamination | Agreed inspection around entry and exit | Risk-based sample rate and acceptance boundary |
| Heat and buildup | Bore appearance, tool condition, cycle count | Process window and cleaning rule |
| Tool wear | Edge or rim condition at planned intervals | Replacement limit before hole failure |
| 包装 | Edge protection, size separation, labels | Shipment inspection against approved layout |
A Drill Bit can pass diameter inspection and still fail the laminate-quality requirement. Conversely, a clean one-off hole does not prove repeatability if the tool identity, fixture, cycle count, and process conditions are missing. The release record must connect both kinds of evidence.
Batch Consistency Depends on a Defined Change Limit
Repeat supply needs a stable identity. The released Drill Bit record can include material or abrasive direction, critical dimensions, point or rim geometry, shank, surface condition, marking, packaging, inspection method, and functional sample test. Not every manufacturing detail belongs on a customer drawing, but the characteristics that control fit and hole quality need an agreed boundary.
Incoming material control, forming or heat treatment where applicable, grinding or abrasive application, dimensional inspection, surface review, runout sampling, and functional cutting checks protect different parts of the result. A certificate alone cannot show whether the tool cuts the approved fiberglass panel cleanly. The retained reference sample connects factory measurements to application performance.
A Drill Bit supplier should also define how controlled changes are handled. A change in material source, edge preparation, abrasive specification, adapter, packaging, or subcontract process may require internal validation or customer resampling, depending on the released agreement. Bestwin can link revisions to the order and prevent a familiar product name from hiding a functional change.
Packaging matters because a chipped edge or damaged abrasive rim can spoil the first production hole. Tools should be separated, restrained, and labeled so that sizes and approved variants remain identifiable. Receiving inspection can then compare the shipment with the approved layout before tools reach the machine.
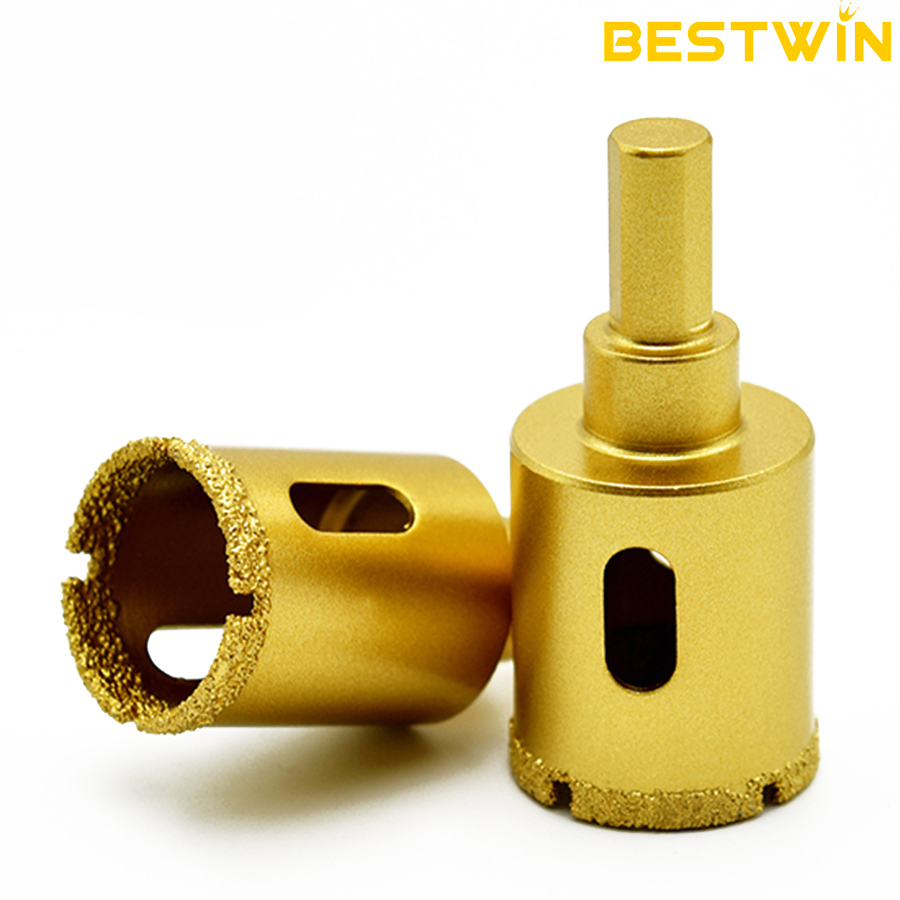
The official brazed diamond hole-saw product image shows another annular form that may be evaluated for suitable abrasive-cutting applications. Its presence here illustrates product construction only; final fiberglass suitability, connection, diameter, process, and lifetime require sample confirmation.
Send Bestwin the Panel and Hole Conditions
An effective RFQ gives the factory a reproducible application rather than only a diameter list. Include representative panel pieces, laminate and gelcoat information, thickness range, hole drawing, entry and exit criteria, permitted delamination, machine and holder, available speed and feed range, fixture and backing, dust method, target tool life, annual demand, set composition, marking, packaging, and applicable standards.
If the program covers several panel constructions, identify the hardest or most damage-sensitive case and do not merge results without evidence. A tool approved on a resin-rich cover may not hold the same limit in a high-fiber structural plate. Bestwin can prepare ドリルビット samples for the defined cases and keep their identities separate through evaluation.
After approval, the project file should hold the tool specification, sample lot, panel lot or reference coupon, machine and fixture revision, process window, hole photographs, dimensional results, wear limit, packaging layout, and change rule. That record lets Bestwin connect manufacturing, inspection, OEM marking, and repeat orders to the same evidence.
Clean Fiberglass Holes Are a Controlled Production Result
Clean fiberglass holes come from controlling how the edge enters, cuts abrasive fibers, carries dust, limits heat, and breaks through a supported laminate. The Drill Bit is central, but panel construction, machine runout, holder, fixture, backing, process stability, inspection, and wear limits determine the finished result.
Bestwin can match ドリルビット products after reviewing the actual composite, hole function, equipment, acceptance criteria, and batch needs. With representative samples and a retained release record, the factory and customer can move from a promising first hole to consistent production without overstating what any single catalog label can guarantee.










 English
 العربية
 Français
 Português
 Português do Brasil
 Italiano
 简体中文
 繁體中文
 日本語
 한국어
 Deutsch
 Español
 Slovenčina
 ไทย
 Türkçe