
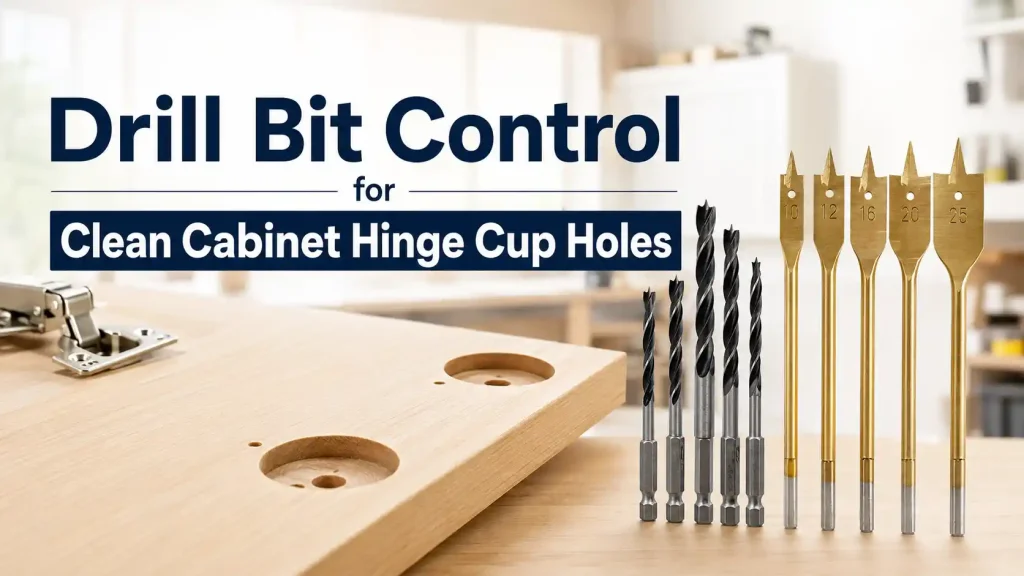
A 35 mm concealed-hinge cup hole looks simple until a cabinet door reaches assembly. A shallow bore leaves the hinge proud, an extra millimeter can mark the face, edge breakout weakens the fixing screws, and a tilted hole changes the door gap. At Bestwin, we manufacture hole-making tools for cabinet factories, furniture OEMs, hardware-kit producers, and distributors, and we match each Drill Bit direction to the panel, hinge drawing, spindle, boring cycle, finish limit, and production quantity. The goal is a flat, repeatable cup seat that lets the hinge install without operator correction.
Respuesta rápida
A Broca produces consistent cabinet hinge cup holes when its diameter, cutting geometry, point or center design, runout, spindle interface, speed, feed, depth stop, chip clearance, and wear limit are validated on the actual panel. For the familiar 35 mm concealed hinge, the nominal diameter is only one requirement. The hole must also have the correct depth, a sufficiently flat bottom, clean entry, controlled edge distance, and adequate remaining material above the door face. We sample MDF, particleboard, plywood, or solid wood separately, inspect a sequence of holes rather than one fresh-tool result, and retain the approved setup with the production identity.
Bestwin connects the cutting result to a controlled tool specification that can be reproduced for the order. That makes the hinge-boring operation a manufacturing process rather than a trial-and-error adjustment on the assembly line.
Start With the Hinge and Door Drawing
Muchas bisagras ocultas para gabinetes utilizan una cazoleta de 35 mm, pero eso no hace que cada instalación sea idéntica. El dibujo del proveedor de la bisagra define el diámetro de la cazoleta, la profundidad de la perforación, el retroceso desde el borde de la puerta, el patrón de los agujeros de fijación y cualquier característica de localización. Las bisagras de solape, embutidas, de medio solape, de cierre suave, para puertas gruesas y de ángulo especial pueden tener una geometría diferente alrededor de la cazoleta. Se debe seleccionar una broca del dibujo de herrajes actual, no de un estándar de taller recordado.
The door drawing adds material thickness, face finish, edge banding, profile, frame geometry, and the distance to rails, glass inserts, or routed details. On a thin door, the remaining face material below the cup can be small. On a profiled door, the back surface may not be parallel to the show face. On a five-piece construction, the cup can cross a joint or approach the stile edge. These conditions change Drill Bit support and breakthrough risk.
We translate the drawing into measurable acceptance points: finished diameter, depth, bottom shape, entry-chip limit, cup perpendicularity, center position, edge distance, fixing-screw engagement, and face-mark limit. The hinge is then installed in sampled holes. A gauge can approve size, but only the actual hardware confirms that the cup seats, the flange lies flat, and the door adjustment remains within its intended range.
MDF, Particleboard, Plywood, and Solid Wood Cut Differently
MDF is uniform but can generate fine dust and lose edge strength if the tool rubs or becomes dull. Particleboard contains larger chips and resin; the entry can crumble and the cup wall can tear around coarse particles. Plywood alternates grain direction and adhesive layers, so the Drill Bit sees changing resistance through the depth. Veneered panels add a thin cosmetic layer that may lift or splinter even when the substrate looks acceptable.
Solid wood adds grain direction, density variation, moisture content, and possible knots. A clean Drill Bit result in straight-grained poplar does not qualify the same setup for oak, beech, rubberwood, or a resinous softwood. Laminated and coated panels add a surface whose chip boundary can be more important than the substrate. We ask for identified production panels or representative offcuts and keep the material source with the sample record.
Panel condition matters too. Moisture, storage temperature, warpage, and surface contamination can influence clamping and cutting. A production sample should represent the normal conditioning route. If several suppliers or board grades will be used, the plan includes the most chip-prone and the hardest-to-cut variants rather than approving the easiest panel.
Control the Machine Before Blaming the Drill Bit
Spindle runout, chuck condition, collet cleanliness, adapter stack, quill play, and table alignment all affect the finished cup. A perfectly ground Drill Bit cannot produce a round, perpendicular bore when the spindle axis moves. Conversely, a worn tool can be hidden temporarily by a rigid machine and generous hinge clearance. We separate machine contribution from tool contribution during setup.
Runout is checked near the cutting end after the tool is mounted by the released method. The panel support is checked for deflection, and the spindle is verified perpendicular to the reference face. On a line-boring machine, neighboring heads and stops can influence clamping or positioning. On a CNC router, holder balance, stick-out, interpolation settings, and program coordinates enter the record. On a drill press or hinge-boring machine, fence, stops, clamping, and depth mechanism are equally important.
El Broca category gives buyers a wider view of Bestwin hole-making products, but the approved hinge-cup tool retains its own diameter, shank, rotation, length, geometry, and operating window. A similar-looking wood bit should not be substituted without repeating the relevant checks.
Define a Hinge Cup Hole as More Than 35 mm
Un diámetro nominal de 35 mm debe encajar en la copa sin interferencia o movimiento excesivos. Si el orificio es demasiado pequeño, el instalador puede golpear la bisagra o rayar la pared. Si es demasiado grande, los tornillos de fijación soportan más carga y la alineación puede moverse durante el apriete. La base debe ser lo suficientemente plana para el cuerpo de la bisagra, mientras que cualquier punto central o rebaje debe permanecer dentro del espacio disponible del herraje.
Depth is especially critical. Too shallow and the flange does not seat; too deep and the remaining face layer becomes weak or visibly marked. The control plan should state the permitted depth range and how it is measured. A depth gauge, machine position record, or go/no-go fixture can support inspection. The first-piece check should include the actual hinge and fixing method.
Table 1. Cabinet Hinge Cup Hole Requirements and Production Evidence
| Requirement | Project input | Sample evidence | Release focus |
|---|---|---|---|
| Cup diameter | Current hinge drawing and fit allowance | Bore gauge or measured diameter at multiple directions | Cup seats without force or excess play |
| Bore depth | Hinge body depth and door thickness | Depth readings plus remaining-face calculation | Flange sits flat without face marking |
| Calidad de entrada | Veneer, coating, laminate, or wood-fiber chip limit | Standard-light photographs with scale | Damage remains inside the covered boundary |
| Bottom geometry | Hinge body and center clearance | Profile inspection and installed-hinge check | No rocking, obstruction, or proud flange |
| Position and axis | Setback, edge distance, fixing-hole pattern | Stop or CNC record, axis check, assembly measurement | Door gap and adjustment stay within target |
| Tool life | Expected doors per shift and inspection interval | Sequential-hole log, cut time, wear photographs | Quality remains stable through the agreed interval |
The acceptance record should state which face is the reference and whether the door is drilled before or after edge banding. If the setback is measured from an unfinished edge but the assembly uses a finished edge, the cup can shift relative to the cabinet. Drill Bit control cannot correct a reference error in the production drawing.

Match Cutting Geometry to the Cup, Not Just the Material
Hinge cup boring normally needs a wide, flat-bottomed hole with controlled entry. A Forstner-style or purpose-designed hinge-boring geometry can use a rim and internal cutting edges to establish the circumference and remove the center. The exact point, rim, flute, relief, and carbide or steel construction depend on material, machine, life target, and cost. A Drill Bit intended for deep chip transport or general through-holes may not create the required cup bottom.
El diseño central afecta la estabilidad de arranque y la holgura inferior. Una punta central larga puede ubicarse bien pero dejar una marca más profunda. Una punta corta puede preservar la parte inferior pero puede requerir una mejor guía de la máquina. La geometría del borde influye en el rayado y la fuerza de corte de la chapa. Los cortadores internos influyen en la superficie inferior y la formación de virutas. Evaluamos la forma completa con la bisagra del cliente en lugar de describir una característica como universalmente mejor.
Rotation direction and spindle arrangement must be explicit. Multi-spindle woodworking machines may use left- and right-hand tools. Installing the wrong Drill Bit rotation can damage the tool, panel, and machine. Shank diameter, flat or set-screw feature, overall length, working length, and reference shoulder must match the holder and depth-setting method. These dimensions become controlled characteristics for repeat orders.
Entry Quality Begins With Support and a Stable Start
The visible face may be on the opposite side of the drilling operation, but entry damage on the back can still extend beyond the hinge flange or weaken the screw area. Veneer and laminate need clean scoring before fibers or coating are lifted. A Drill Bit with a damaged rim, excessive runout, or unstable start can tear the surface before its internal edges begin removing material.
Panel support should keep the door flat without crushing a finished face. Stops and clamps must resist the lateral and axial forces of the Drill Bit cut. A warped door that rocks on the table changes depth and axis. Vacuum pods on CNC equipment must be positioned so that the panel does not flex near the cup. For manual jigs, the guide must sit flat and resist walking.
We inspect the entry under consistent light and compare damage with an agreed boundary. “Looks clean” is difficult to reproduce across shifts. A photograph with a scale, maximum-chip example, or go/no-go overlay makes the rule easier to train and audit. The same inspection is repeated after the Drill Bit has completed enough holes to represent production wear.
Depth Control Must Include Tool and Machine Tolerances
A mechanical stop can move, a CNC tool length can be entered incorrectly, and a replaceable insert or reground tool can change effective length. The depth plan should define the reference surface, tool datum, offset method, first-piece check, and verification interval. A Drill Bit supplied to a repeat customer must also retain the relevant length and shoulder dimensions within the agreed control.
Door thickness variation is part of the risk. A constant bore depth leaves less face material in a thinner panel. Incoming panel checks should therefore be connected to the drilling plan. If the permitted thickness range is wide, the machine may need recipe control or the product drawing may need a larger safety allowance.
Do not use the first visible face dimple as the only depth warning. By then, the panel may already be scrap. Calculate remaining material from the minimum door thickness and maximum Drill Bit cup depth, then prove it on samples. For high-value finished fronts, non-destructive first-piece checks and controlled tool offsets reduce the chance of a batch-wide error.
Speed and Feed Need a Reproducible Window
Spindle speed affects rim velocity, cutting heat, chip shape, and finish. Feed affects cutting load, rubbing, bottom quality, and cycle time. Too fast a feed can tear the entry or deflect a weak setup. Too little effective feed can cause rubbing, heat, resin build-up, and premature dulling. One speed copied from another diameter or material is not a complete Drill Bit instruction.
During Drill Bit samples, we record machine model, holder, spindle setting, loaded behavior where available, feed rate or travel time, peck or dwell behavior, extraction, panel construction, and hole sequence. We seek a window that produces acceptable holes without abnormal noise, burning, severe vibration, packed chips, or operator rescue. The chosen production value sits inside that window rather than at its edge.
Para una taladradora neumática de bisagras, la presión del aire y la condición de control de avance afectan el movimiento real. Para una taladradora manual, la fuerza del operador es menos repetible, por lo que las paradas, la guía y una expectativa de tiempo ayudan. Para CNC, el programa y el número de herramienta se pueden bloquear en el registro aprobado. En todos los casos, la broca se evalúa en el equipo que creará los agujeros del pedido.
Chip Extraction Protects the Rim and Bottom
A wide cup creates a large volume of chips in a short travel. If chips remain in the bore, they can be recut, increase heat, mark the wall, or pack around the internal cutters. MDF dust and particleboard fragments behave differently. Extraction airflow, nozzle position, flute path, and machine cycle all affect clearance.
We inspect the bore and Drill Bit between controlled intervals. Resin or adhesive build-up can make a sharp edge behave like a dull one. Cleaning should use a method compatible with the tool material and any brazed or bonded construction. A production instruction defines when to inspect and clean, rather than waiting for visible smoke or a rejected door.
El aire comprimido no debe tratarse como un sustituto informal de una extracción de polvo adecuada. El polvo fino de madera crea problemas de salud, limpieza y combustión que deben incluirse en los controles de riesgo de la fábrica. La prueba de la herramienta registra el sistema de extracción, pero la protección de la máquina del cliente, el sistema de control de polvo y los procedimientos del lugar de trabajo siguen siendo esenciales.

Not Every Wood Bit Is a Hinge Cup Bit
Wood-drilling families solve different jobs. Twist bits can make pilot or fixing holes. Brad-point tools can improve location and edge control in appropriate diameters. Spade bits make relatively fast general holes. Auger designs use a screw point and open spirals to pull through deeper wood. A 35 mm hinge cup needs its own flat-bottom, depth, and finish behavior. Similar diameter does not mean similar function.
The auger product image shown above is useful as a comparison because its lead screw and long chip-carrying flutes reveal a different purpose. It can be relevant to deep timber holes or other cabinet-production tasks, but it should not be represented as the approved tool for a shallow concealed-hinge seat. Matching the Drill Bit geometry to the hole prevents purchasing teams from grouping every black-finished wood tool under one interchangeable description.
This distinction also matters in mixed OEM kits. A cabinet hardware kit may include cup boring, pilot drilling, shelf-pin drilling, confirmat screws, or cable openings. Each hole should have a named tool position and controlled dimensions. Bundling tools for commercial convenience must not erase their separate functional specifications.

Edge Distance and Fixing Holes Must Be Validated Together
La cazoleta se sitúa cerca del borde de la puerta, y los tornillos o espigas de fijación de la bisagra ocupan el mismo material local. Si la cazoleta está demasiado cerca, la pared puede romperse hacia el borde. Si está demasiado lejos, la geometría de la bisagra cambia el solape y el rango de ajuste. Una broca que realiza un orificio aislado excelente puede seguir siendo inadecuada cuando el patrón de fijación completo elimina demasiado material. Por lo tanto, la aprobación de la broca incluye el patrón de fijación real.
We drill the cup and fixing pattern in their production sequence, install the hinge, tighten it using the released method, and inspect for cracking, swelling, stripped fibers, or flange movement. Particleboard density near an edge can be less forgiving than the center of a test coupon. The sample should use a full-width door strip or a coupon that reproduces the real edge support.
Edge banding changes the reference and can add local adhesive or heat effects. Drilling before banding may expose the cup wall to later handling; drilling after banding requires a reliable reference from the finished edge. The routing choice is recorded so that a successful Drill Bit sample is not transferred to a different production sequence without review.
Inspect Wear Before Holes Become Rejects
A fresh tool often creates the best entry and shortest cycle. Production approval must show how quality changes as the rim and internal cutters wear. We log hole number, panel identity, cycle time, diameter, depth, entry damage, bottom condition, sound, spindle load if available, and visible tool condition. The sequence continues through the proposed inspection or replacement interval.
Las señales útiles de parada de la broca incluyen virutas fuera del límite permitido, aumento del tiempo de corte, quemaduras, desviación del diámetro, un fondo rugoso o sobresaliente, vibración anormal y daños visibles en el filo. Un número fijo de agujeros puede simplificar la planificación, pero debe estar respaldado por evidencia del material del cliente. Diferentes contenidos de resina o laminado pueden cambiar la vida útil.
Regrinding may be possible for some constructions, but it changes geometry and dimensions and must be controlled. The customer should know the permitted service route, identification after service, and acceptance check. A reground Drill Bit should not return to the line based only on visual sharpness.
Use Defect Location to Guide Troubleshooting
Entry chipping points toward rim condition, runout, support, surface construction, or starting stability. A tapered or oval wall suggests axis error, deflection, holder movement, or tool-body geometry. A rough bottom can indicate internal-edge wear, chip packing, feed, or depth-stop bounce. Face marking suggests excessive depth, thin material, panel deflection, or a center feature with insufficient clearance.
Burning or resin build-up can involve speed, low effective feed, dull Drill Bit edges, extraction, or panel adhesive. Sudden noise may come from a loose holder, damaged tool, knot, foreign inclusion, or spindle issue. We avoid changing the Drill Bit specification until the machine, panel, and process evidence are separated. Otherwise, one correction can hide the fault while creating a new one.
The general definition and variety shown for a Broca help explain why cutting tools are classified by geometry and intended work. In cabinet production, the practical selection still depends on the hinge seat, panel construction, machine interface, and controlled sample.
Sample Approval Must Represent a Production Shift
One perfect cup made slowly by an engineer is not a production result. The sample plan uses normal clamping, extraction, cycle time, and operators or machine program. It includes start-up checks, repeated holes, tool cleaning if intended, panel changes, and the inspection interval. A Drill Bit is approved when the process remains within the agreed hole limits without hidden manual correction.
Capability can be assessed on diameter, depth, and position where the measurement system is suitable. Cosmetic entry quality and bottom finish may use approved boundary samples. The hinge installation result remains a final functional check. If the line drills two or more cup positions per door, both positions and the worst support condition are represented.
The retained Drill Bit record includes tool specification, machine, holder, program or stop settings, panel identity, hinge drawing revision, results, photographs, and approved samples. For repeat purchasing from Drill Bit Suppliers, this record provides a concrete comparison and prevents a low-information quotation from becoming an unplanned process change.
Manufacturer Control Supports Repeatable Cabinet Output
At Bestwin, our work as a Drill Bit supplier includes reviewing the application data, agreeing the sample construction, manufacturing to the controlled specification, and connecting inspection to the order identity. Diameter, shank, rotation, overall length, working geometry, material or carbide direction, marking, packaging, and agreed test points are recorded according to project scope.
For a cabinet OEM comparing a Drill Bit manufacturer, retained hinge-fit evidence and a stable revision identity are more useful than a nominal diameter alone.
Bestwin matches the sample direction to the hinge drawing, panel construction, machine interface, and production life target. Bestwin supports the release with agreed inspection, marking, packaging, and repeat-order controls.
Packaging protects the Drill Bit cutting rim, center feature, shank, and reference surfaces from contact and corrosion during shipment. Mixed left- and right-hand tools or several diameters need clear separation and labeling. A factory-approved tool that reaches the customer with a chipped rim is not the same production input.
Change communication should be agreed for OEM programs. A material, geometry, process, or sub-supplier change can affect life, finish, certification files, or machine settings even when the nominal diameter is unchanged. A stable purchasing relationship with Drill Bit Suppliers depends on controlled samples and transparent revision identity, not only on unit price.
The second internal Broca reference is a useful starting point for product-family discussion. The quotation should still identify the exact hinge, material, machine, dimensions, life target, packaging, and evidence required for release.
What to Send With an RFQ
Send the hinge maker and drawing revision, nominal cup diameter, depth tolerance, setback, fixing-hole pattern, door thickness range, material construction, veneer or coating, edge-band route, cosmetic chip limit, annual quantity, holes per shift, machine type, spindle rotation, holder or shank, speed range, feed method, extraction, depth reference, inspection method, expected tool life, regrinding policy, marking, and packaging requirements.
Photographs help, but include a representative panel and hinge when practical. A retained sample allows our engineering and production teams to compare entry, wall, bottom, fit, and face condition. If the current process has rejects, provide the hole sequence, tool age, machine, settings, panel batch, defect position, and whether the issue appears at start-up or after warming.
When comparing Drill Bit Suppliers, ask each bidder to state assumptions and sample boundaries. A price attached only to “35 mm wood bit” cannot establish fit, depth, rotation, life, finish, or repeatability. A detailed RFQ reduces quotation ambiguity and shortens sample correction.
Preguntas frecuentes
Is every 35 mm wood bit suitable for concealed hinges?
No. The nominal diameter does not establish bottom geometry, center clearance, entry quality, runout, shank, rotation, or production life. The tool must be tested with the actual hinge, panel, machine, and depth requirement.
How can we prevent a cup hole from showing on the door face?
Control the maximum drilling depth against the minimum panel thickness, keep the panel supported, verify tool length and machine datum, and inspect the first piece. Leave an agreed remaining-face margin and account for panel variation rather than relying on a visual warning.
Why do holes become rough after a good first batch?
Rim or internal-edge wear, resin build-up, packed chips, holder movement, extraction changes, or panel variation can appear over time. Track hole number and cycle data, inspect at a defined interval, and compare defects by location before changing the tool or settings.
Should a cabinet factory use a jig, drill press, hinge borer, or CNC?
Any of these can work when it provides the required position, axis, depth, support, and repeatability at the production volume. The approved Drill Bit and operating window should be validated on the chosen equipment rather than transferred from a different machine without checks.
Conclusión
Clean cabinet hinge cup holes come from a controlled combination of hardware drawing, panel, tool geometry, machine condition, speed, feed, depth, support, extraction, and wear limits. A Drill Bit selected only by its 35 mm label leaves the most important assembly risks unresolved.
Bestwin helps cabinet manufacturers and distributors convert those risks into a practical sample and repeat-order specification. When the cup seats flat, the face remains intact, the edge stays strong, and a production-length sequence holds the same result, the boring tool becomes a dependable part of cabinet assembly rather than a source of rework.










 English
 العربية
 Français
 Português
 Português do Brasil
 Italiano
 简体中文
 繁體中文
 日本語
 한국어
 Deutsch
 Español
 Slovenčina
 ไทย
 Türkçe